

By understanding a little bit extra concerning the 3D printing course of, and the way settings in MatterControl have an effect on extrusion, we may also help you scale back and even get rid of oozing and stringing out of your 3D prints. This needs to be part of the common upkeep and calibration program in your 3d printer.
Maybe the most typical query we get from new 3D printer homeowners is, “How do I eliminate oozing and stringing on my prints?”
Extruding thermoplastic is a sophisticated course of with dozens of variables in play. Nevertheless, understanding what causes oozing/stringing in your prints doesn’t should be that difficult.
What’s Retraction?
First, let’s begin with the most typical false impression about what retraction does and the way it works.
Fantasy – Retraction “sucks” filament again up via the recent finish. So, the extra retraction you employ, the much less oozing you’ll get.
Reality – As soon as filament has melted within the “soften zone” of your scorching finish, it can’t be retracted. Retraction doesn’t create unfavourable strain. Scorching ends are usually not sealed/hermetic. In the event that they had been, then the unfavourable strain would “suck” molten filament again up via the recent finish. This could probably result in numerous jams and different extrusion points, however this isn’t the case.
Take into consideration candle wax. When you had been to place a small cylinder of wax right into a pool of melted candle wax after which pull it out, would the melted wax include it? In fact not. Whereas a small quantity of wax will follow the cylinder whenever you take away it, it doesn’t pull the pool of molten wax up with it.
In the identical approach, the stable filament above the soften zone doesn’t retract the molten filament with it.
Okay, so if retraction doesn’t pull filament again up via the nozzle, what does it do?
The aim of retraction is solely to alleviate strain from the soften zone in order that filament isn’t being pressured via the nozzle throughout non-print strikes.
What are the Finest Retraction Settings?
There’s lots of misinformation on the market about how a lot retraction it’s best to have. I’ve seen suggestions from .1mm all the way in which as much as 20mm. So what’s the right amount?
The correct quantity is the minimal quantity required to cut back probably the most stringing in your half. Some machines and scorching ends require extra retraction than others, and every materials has totally different necessities. Usually, although, it’s unlikely it’s best to want greater than 5mm or lower than 1mm.
Settings to Tune
There are a number of different essential settings that have an effect on oozing/stringing on components. We’ll undergo the method of adjusting your machine to get the least quantity of oozing doable, however it’s critically essential that you just begin out with a correctly calibrated extruder. When you haven’t calibrated your extruder earlier than, learn tips on how to calibrate your extruder earlier than you begin adjusting retraction settings.
There are solely 2 settings we’ll be adjusting for retraction on this article:
- Retraction: Size on Transfer
- Pace: Journey (velocity for non-Print strikes)

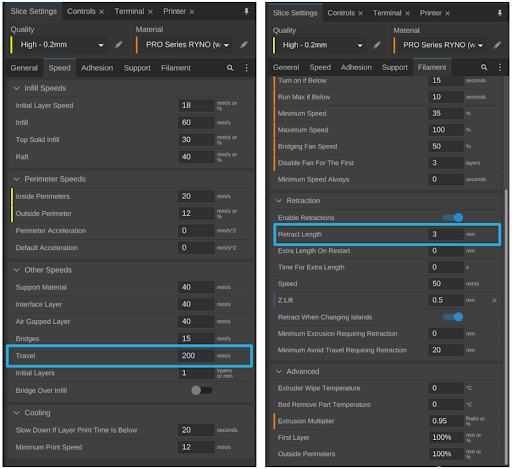
There are definitely different settings that have an effect on oozing, however these are a very powerful, and the best to check and alter. We’ll cowl the opposite settings in a future article.
We created a easy STL (Obtain the file right here) to point out the consequences of various settings on oozing/stringing. They’re 10mm cubes and they’re spaced 10mm, 20mm, and 40mm aside. The check machine was a SeeMeCNC Rostock Max with an E3D v6 scorching finish. The filament used was MatterHackers commonplace blue PLA.
These settings had been used for all check prints:
- Layer Top: 0.25mm
- Infill: 25% – Triangle
- Perimeters: 2
- Stable High Layers: 2
- Stable Backside Layers: 2
- Infill and Perimeter Speeds: 40mm/s
- All components had been printed with a skirt, however the skirt was eliminated for a few of the footage so as to extra clearly visualize the oozing/stringing
Begin Dialing within the Settings
This print had 0 retraction and 40mm/s journey velocity (non-print strikes). This represents concerning the worst oozing/stringing doable on this machine
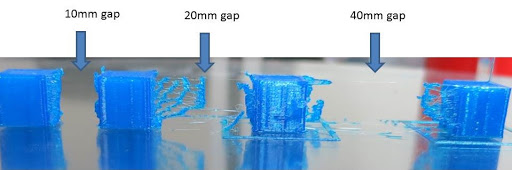
You’ll discover that the stringing between the 20 and 40mm gaps are a lot worse than the 10mm. That is just because there’s extra time for filament to ooze out of the recent finish. This is the reason journey velocity for non-print strikes performs a giant half in oozing/stringing. The sooner you’re in a position to transfer to the following print place, the much less time there may be for filament to ooze from the recent finish.
With this as the place to begin, the very first thing to do is to extend the journey velocity of non-print strikes. Each machine has totally different limitations, however 150-250mm/s is the probably the vary your machine can deal with nicely. There actually received’t be a noticeable distinction in stringing between 150 and 250mm/s due to acceleration and different limits within the firmware, however that’s for one more article.
This print had 0 retraction, however the journey velocity was elevated from 40mm/s to 150mm/s.
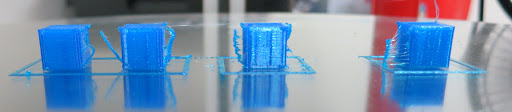
It’s higher than the earlier print, however clearly not acceptable.
As soon as the journey velocity is about, we’ll enhance the retraction distance. Once more, the purpose is to make use of the minimal quantity of retraction obligatory. Utilizing greater than obligatory could cause jams, blobs, and different extrusion associated points.
This print has 1mm retraction with 150mm/s journey velocity:

There’s clear enchancment – particularly within the 10mm hole – however nonetheless lots of stringing between components
Subsequent, 2mm retraction, 150mm/s journey velocity:
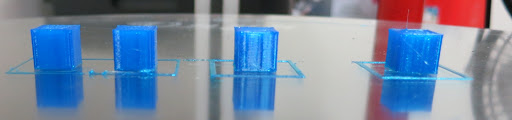
Nearly proper. There are a number of very, very advantageous strands of PLA which you’ll not even have the ability to see within the image, however the edges and faces are all very clear with no blobs or extra filament to talk of.
We’re not carried out but, although. We’ll enhance the retraction to 3mm to see if there may be any noticeable enchancment.
3mm retraction, 150mm/s journey velocity
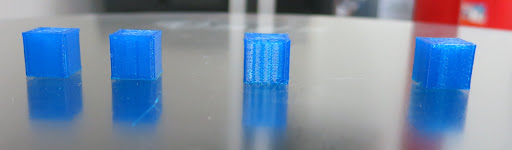
Excellent! No stringing, no oozing. Simply completely printed cubes.
So, it seems to be like 3mm is the correct quantity of retraction for PLA on this machine.
To rapidly and simply tune your settings to realize optimum retraction, obtain the dice retraction print retraction cubes, and print it together with your present settings.
Based mostly in your outcomes, alter both the journey velocity or the retraction distance and reprint. Solely change 1 setting at a time. That approach, you’ll be able to simply see the impact of every change.
Alter your retraction distance up/down by both 0.5 or 1mm increments. We do not suggest distances larger than 5mm, or lower than 0.5mm.
Lastly, you might have to carry out this check and alter for various supplies. Some supplies could ooze greater than others, and will require elevated retraction distance & journey velocity to realize the identical outcomes.
Comfortable Ooze-Free Printing!