


Discover these important steps which can be required for getting the most effective metallic 3D printed components attainable.
Up to date on August 22, 2023
by
Visitor Contributor Ahead AM
When beginning a printing course of, the objective is to get the very best remaining half. Nonetheless, with a view to obtain that, it’s important for sure pointers to be revered. On this article, we are going to contact on the necessary steps required to provide the very best printed metallic half with BASF Ahead AM’s Ultrafuse® Steel materials. Let’s start with the guidelines and tips to efficiently print utilizing BASF Ahead AM Ultrafuse® Steel.
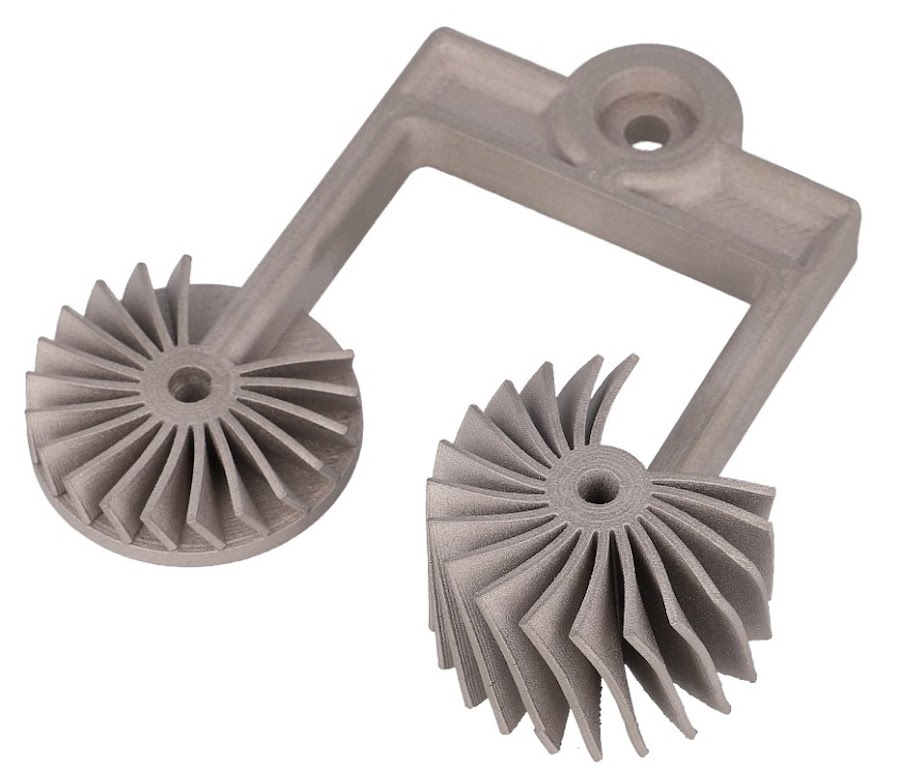
You may discover ways to efficiently print with actual metallic in your desktop 3D printer!
What are Ultrafuse® Steel Filaments?
Ultrafuse® Steel filaments are metal-polymer composite filaments particularly designed for Fused Filament Fabrication (FFF) printing. The non-slip outer floor of Ultrafuse® filaments has been optimized for printing on each Bowden and direct drive FFF extruders. With excessive metallic contents of round 90% by mass, mixed with even distribution of tailored metallic powders throughout the binder matrix, Ultrafuse® metallic filaments present each reliable efficiency and assist to cut back the chance of printing defects, subsequently, growing remaining half success charges.
When in comparison with different nice metallic powder strategies like Selective Laser Melting (SLM), Direct Steel Laser Sintering (DMLS), Direct Steel Deposition (DMD), and Binder Jetting, Ultrafuse® filaments bind metallic particles inside a strong polymer system at excessive density to cut back doubtlessly dangerous nice metallic particle publicity. And since there isn’t a have to unpack the printed components out of uncooked powder throughout the construct chamber, operators have minimal publicity to nice metallic particles.
BASF Ahead AM presents two metallic filaments as a part of its portfolio: Ultrafuse® 316L and Ultrafuse® 17-4 PH.
Which results in the query, when do you have to use what materials? Ultrafuse® 17–4PH is the cost-effective, all-rounder stainless-steel, reveals excessive mechanical load resistance and is appropriate for nearly all metallic purposes, solely overwhelmed by Ultrafuse® 316L relating to corrosion resistance. If you wish to examine which half is produced from 316L or 17-4 PH, merely use a magnet. If it sticks, it’s 17-4 PH. If it doesn’t, the half is made out of 316L.
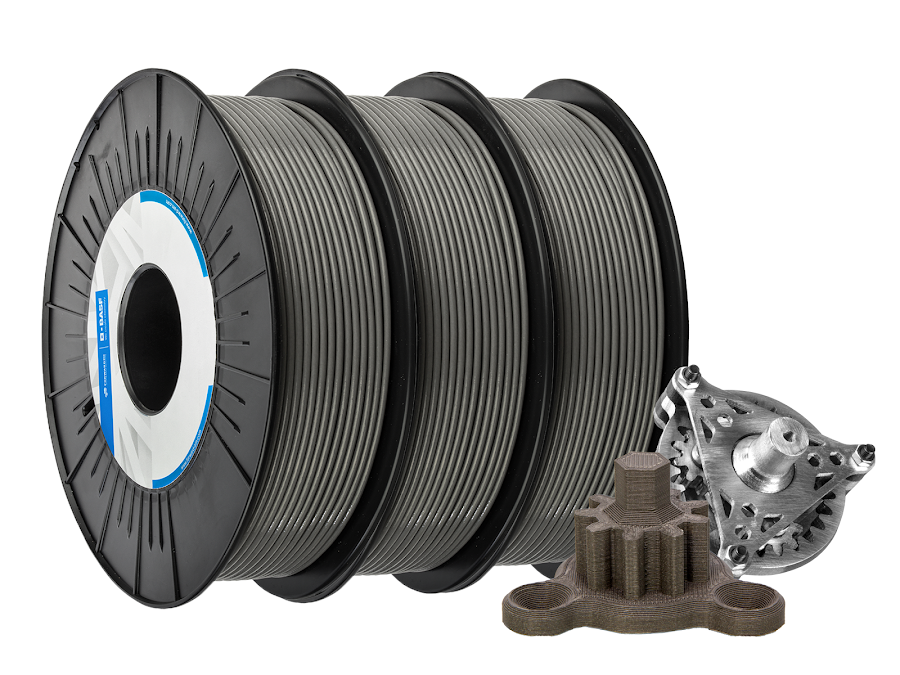
BASF Ultrafuse 316L Steel Filament
Common Necessary Setting and Tips
Earlier than we delve into a very powerful ideas and tips, remember to overview the desk under. In it, you will discover a short abstract of how one can efficiently work with metallic filaments.
Instructed Printing Parameter
The collection of printing parameters throughout the slicing course of is important for half high quality and printing time. The advised parameters seen within the desk under function a place to begin for brand new customers seeking to start printing rapidly. As with every manufacturing course of, every half presents particular challenges and may profit from tuning and optimization with a view to obtain the best attainable high quality.
- Nozzle Measurement: 0.3 – 0.8mm
- Varies relying on the extent of element required and print time
- Line Width: ±10-20% Nozzle dimension
- Retraction Distance: 1.5mm / 5.0mm
- Retraction Velocity: 45 mm/s
- Layer Peak: 0.10 – 0.25 mm
- Not more than 60% of the nozzle dimension is really useful
- Outlines: 1-3
- Too many outlines may end up in wall separation
- Infill Density (Strong Half): 105% Strains
- Rectilinear sorts have proven to provide greater densities
- Infill Overlap: 20-35%
- Overlap between the infill and the partitions should be ensured
- Infill Kind (hole): >60% gyroid, grid, or triangle
- Minimal infill above 60% for greatest outcomes, however decrease values attainable with testing
- Infill Line Route: [45, -45]
- Nozzle Temperature: 235°C – 245°C
- Calibrate to make sure precise temperature matches slicer temperature settings
- Mattress Temperature: 90°C – 105°C
- Calibrate to make sure precise temperature matches slicer temperature settings
- Cooling: None
- Half cooling usually will increase warpage however could be useful throughout bridging
- Max. Print Velocity: 45 mm/s
- Slower printing speeds produce denser, extra correct outcomes
- Extrusion Charge: Max 8cm3/h
- By nozzle dimension 0.4mm decrease charges really useful
- Scaling: XY 120%, Z 124%
- See Shrinkage and Oversizing Issue
Design Tips
Creating and choosing the proper design is essential for a high-quality and purposeful 3D printed object. Additionally it is necessary to do not forget that the rules are sometimes suggestions, not limitations. And plenty of pointers are pushed by the wants of the D&S course of.
- Half Measurement: The utmost inexperienced half footprint can’t exceed X 100, Y 100, Z 100 mm with a view to match on the ceramic plates supporting the components all through debinding and sintering. Bigger components are achievable; nonetheless, they will endure from warpage whereas printing and sometimes require longer improvement occasions. Probably the most profitable dimension for brand new customers is X 60, Y 60, Z 60 mm.
- Unsupported Partitions: To reduce the prospect of collapse and distortion, unsupported wall top to width ratios under 6:1 have been confirmed to be the best. Though simply printed, ratios above 6:1 resulted in cracking and even half collapse.
Mono Extrusion for Steel Solely – 2.5D
- Overhangs: >35°
- Needs to be prevented by the half desigh
- Assist Construction: Necessary for profitable printing
- Assist Materials: Printed from the identical materials
- Assist Elimination: Subtractive removing from the metallic half by way of sawing, milling, drilling, and submitting
- Shrinkage Plate: Probably requires CAD, separate print job, meeting finalized on the D&S service accomplice
- Separatable Dwell setter (assist construction plus shrinkage plate): Requires CAD, separate print job, error-prone finalization of the half meeting
The Large Three
There are three massive subjects that ought to at all times be thought of when printing Ultrafuse® Steel Filaments: Twist and Deformation after Debinding and Sintering, Shrinkage Plate and Inexperienced Half Preparation.
Twist and Deformation after Debinding and Sintering
When utilizing Ultrafuse® Meta Filaments, an unusual characteristic should be used within the slicer. The printing historical past of the person layers leaves an invisible inner stress within the inexperienced half. That is very true for contour-following strains as they introduce a spring-like stress that follows the thermal historical past of the extruded line. Elements with skinny options or many contour strains endure essentially the most from deformation throughout the sintering course of (Determine 2). The trick is to print the contours with alternating instructions. This compensates the for the stress, and the components usually are not deformed after sintering.
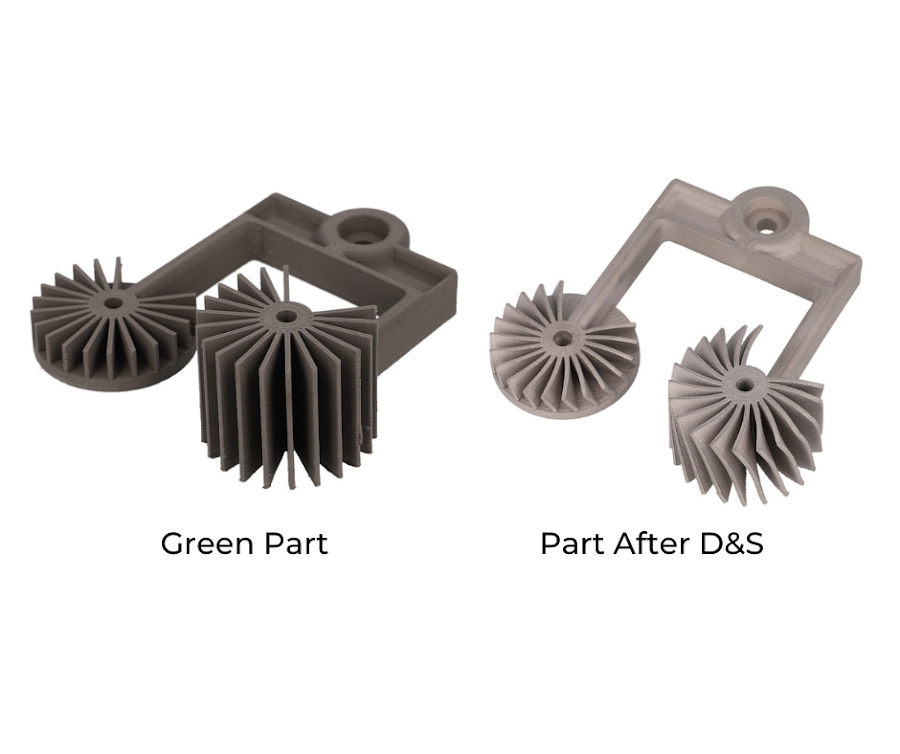
Figures 1&2: Instance of components earlier than and after the debinding and sintering course of.
Shrinkage Plate as a Dwell Setter
The second necessary tip is to pay attention to is the Shrinkage Plate. Through the sintering course of, the metallic particles fuse collectively and as much as 20% shrinkage happens. Throughout shrinkage, the contact space of the half is affected by friction as a counterforce. The coefficient of friction is dependent upon the mass distribution of the half and the design ratios of the half, which seem stretched or deformed (Determine 4). To compensate for the static friction results, a separate plate fabricated from the identical materials, often known as a shrinkage plate (Determine 5), is used to surround the complete contour space of the underside of the half. The specified half sees solely the shrinkage of the plate and no extra static friction. The element leaves the sintering course of freed from distortion and with greater accuracy (Determine 6). For a debinding and sintering service accomplice, the shrinkage plate is coated with a sinter-inactive materials to forestall diffusion and bonding of the shrinkage plate with the specified metallic half.
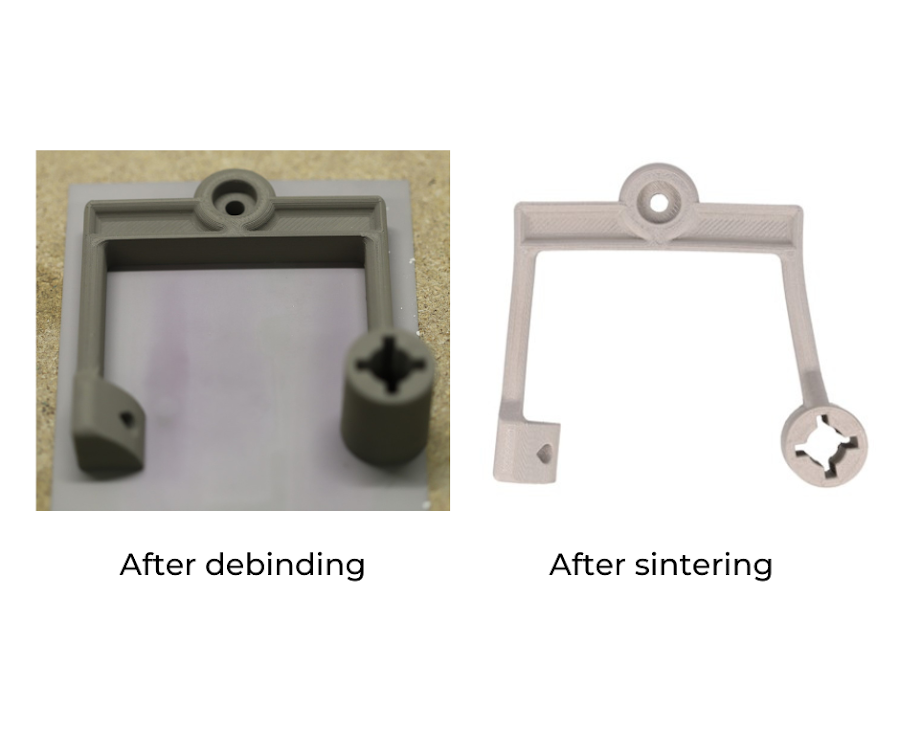
Figures 3&4: A take a look at components after every of the debinding and sintering course of.
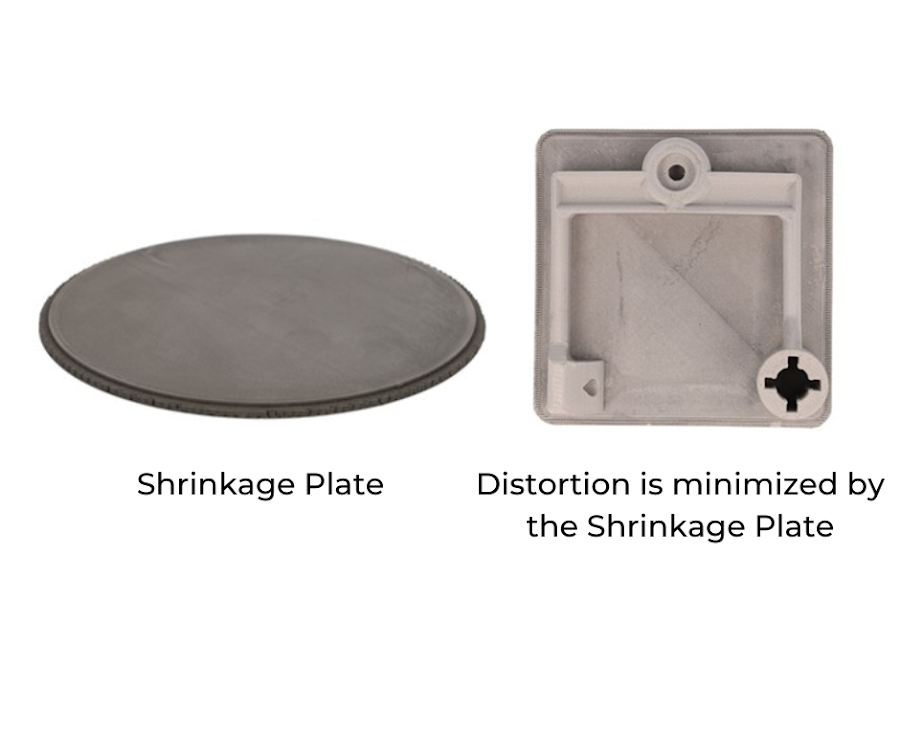
Figures 5&6: Utilizing a shrinkage plate throughout the D&S course of helps decrease half distortion.
Inexperienced Half Preparation
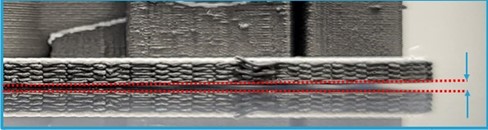
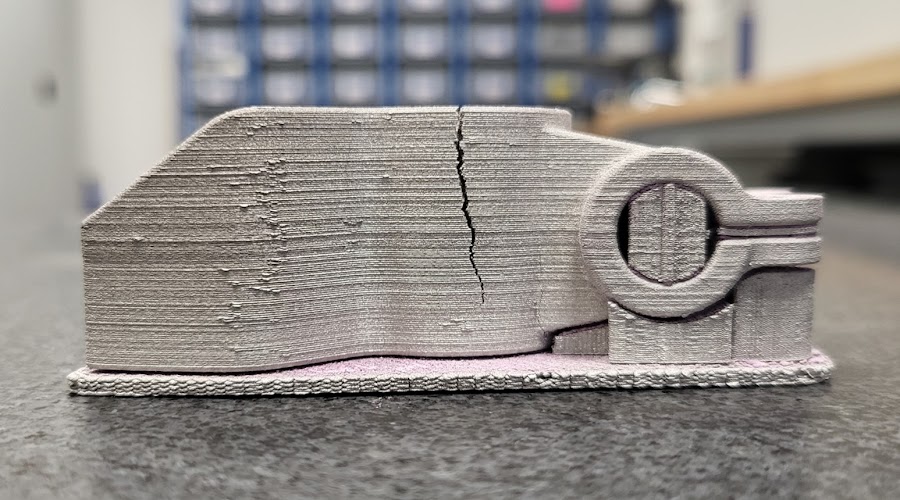
Through the debinding course of, the polymer and thermoplastic matrix is eliminated leaving solely stainless-steel powder with a small quantity of plastic to carry the half’s form. Tiny gaps between the half and the assist floor of the furnace can exert important shear forces on the half, resulting in cracking and collapse. To efficiently survive processing, all half surfaces should be completely planar and flat. A glass print mattress and using Magioo ProMetal are the primary steps in the correct course. Every half ought to be checked for planarity earlier than debinding and sintering and, if crucial, flattened utilizing sandpaper or different subtractive strategies.
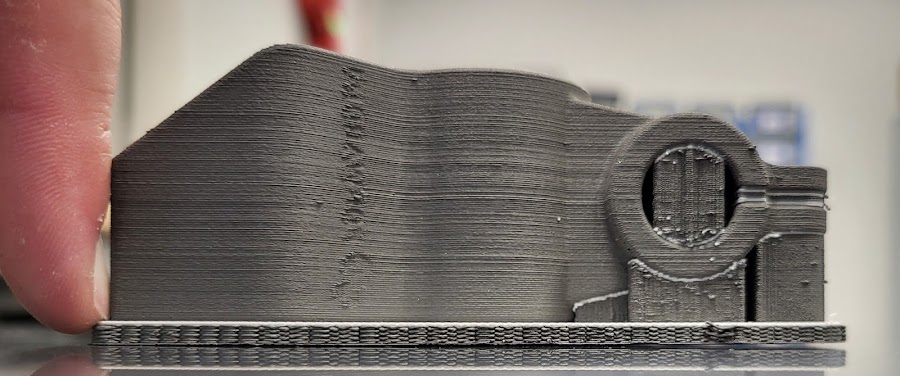
Determine 7: Half after launch from the construct plate
Determine 8: Crack after sintering course of
Determine 9: Little Hole between element and underlaying floor
We hope that by using the following tips and tips, all of your metallic components can be printed as anticipated. For extra data and extra ideas and tips, remember to take a look at BASF Ahead AM’s Steel Person Guideline. Till then, pleased printing!